 EN
💧 Clean Water Pump Engineering Guide for Demanding Installations
Selecting a purpose-built clean water pump requires evaluating dynamic system hydraulics rather than merely matching nominal motor horsepower ratings. Operating environments across commercial agricultural irrigation, industrial fluid transfer, and municipal booster systems demand reliable continuous duty. When a pumping unit encounters excessive head resistance, uncalculated suction lift, or unsuspected particulate abrasive loads, premature mechanical breakdown becomes inevitable.
For mechanical contractors, agricultural engineers, and equipment distributors, sizing an industrial clear water pump begins by mapping real-world system resistance against published manufacturer performance curves. Treating fluid transfer as an interconnected system preserves machinery lifespan, lowers energy expenditure, and prevents costly operational disruptions during peak production cycles.
🌊 Defining Liquid Chemistry and Clear Water Operating Limits
A standard clean water pump is engineered specifically for non-viscous liquids devoid of abrasive suspended solids, corrosive chemicals, or stringy fibrous contaminants. Premature seal erosion and volute scouring frequently occur when clean-water equipment is deployed in settling ponds, untreated surface runoff, or silty canal intakes without proper physical pretreatment.
Fluid Parameter
Clear Water Operational Limits
Engineering Risk Beyond Limits
Recommended Protective Action
Permissible Solids Content
Less than 0.1% by volume, particle diameter under 0.2 mm
Rapid abrasive wear of mechanical seals and impeller vanes
Install multi-stage suction strainers or centrifugal sand separators
Fluid Temperature Range
Typically 0°C to 85°C depending on seal elastomers
Vaporization inside volute leading to severe thermal cavitation
Upgrade to viton elastomers and high-temperature silicon carbide seals
Chemical Acidity / Alkalinity
pH range between 6.5 and 8.5
Chemical pitting of cast iron casings and brass fittings
Specify AISI 304 or 316 stainless steel wetted components
Dynamic Fluid Viscosity
Clean water kinematic viscosity near 1.0 mm²/s
Increased motor drag, drastic head reduction, severe motor overload
Evaluate specialized positive displacement or slurry units
| Fluid Parameter | Clear Water Operational Limits | Engineering Risk Beyond Limits | Recommended Protective Action |
|---|---|---|---|
| Permissible Solids Content | Less than 0.1% by volume, particle diameter under 0.2 mm | Rapid abrasive wear of mechanical seals and impeller vanes | Install multi-stage suction strainers or centrifugal sand separators |
| Fluid Temperature Range | Typically 0°C to 85°C depending on seal elastomers | Vaporization inside volute leading to severe thermal cavitation | Upgrade to viton elastomers and high-temperature silicon carbide seals |
| Chemical Acidity / Alkalinity | pH range between 6.5 and 8.5 | Chemical pitting of cast iron casings and brass fittings | Specify AISI 304 or 316 stainless steel wetted components |
| Dynamic Fluid Viscosity | Clean water kinematic viscosity near 1.0 mm²/s | Increased motor drag, drastic head reduction, severe motor overload | Evaluate specialized positive displacement or slurry units |
When incoming water sources fluctuate following heavy rains or seasonal agricultural runoff, verifying upstream water clarity guarantees that the chosen centrifugal water pump maintains its designed hydraulic tolerances without unexpected wear.
📈 Establishing the Hydraulic Duty Point on Performance Curves
Every reliable pumping project relies on establishing the precise intersection of total system flow demand and Total Dynamic Head (TDH). Selecting equipment based exclusively on maximum headline metrics printed on marketing flyers results in equipment running far outside its intended operating window.
System head calculation encompasses static physical elevation changes, pressure vessel requirements, and cumulative frictional losses across all pipe walls, valves, elbows, and filtration manifolds.
Dynamic Head Element
Sizing Consideration
Field Calculation Formula Impact
Static Discharge Elevation
Vertical rise between pump centerline and highest terminal outlet
Represents constant mechanical lift unaffected by pipe diameter
Friction Head Losses
Drag created along pipe walls, fittings, check valves, and bends
Increases exponentially with excessive fluid velocity in narrow pipes
Terminal Residual Pressure
Operational pressure demanded by drip emitters or spray nozzles
Converted directly into equivalent head (1 bar equals 10.2 meters of head)
Dynamic Suction Lift
Distance from minimum liquid drawdown level to pump intake port
Crucial for calculating Net Positive Suction Head margins
| Dynamic Head Element | Sizing Consideration | Field Calculation Formula Impact |
|---|---|---|
| Static Discharge Elevation | Vertical rise between pump centerline and highest terminal outlet | Represents constant mechanical lift unaffected by pipe diameter |
| Friction Head Losses | Drag created along pipe walls, fittings, check valves, and bends | Increases exponentially with excessive fluid velocity in narrow pipes |
| Terminal Residual Pressure | Operational pressure demanded by drip emitters or spray nozzles | Converted directly into equivalent head (1 bar equals 10.2 meters of head) |
| Dynamic Suction Lift | Distance from minimum liquid drawdown level to pump intake port | Crucial for calculating Net Positive Suction Head margins |
Positioning the operating duty point near the Best Efficiency Point (BEP) ensures smooth laminar flow through the impeller vanes. Running a clean water pump too far to the left of its curve causes radial thrust that deflects drive shafts, while operating excessively far to the right induces severe motor overload and thermal burnout.
⚙️ Selecting the Optimal Pump Configuration
Industrial clear water handling generally divides into three primary mechanical arrangements, each engineered to address specific suction lifts, physical footprints, and pressure demands.
Surface Centrifugal Horizontal Units
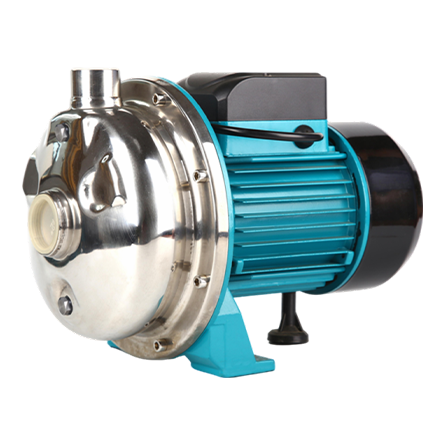
A standard end-suction centrifugal water pump remains the workhorse for flooded suction tanks, canal transfer stations, and factory circulation loops. Its external architecture allows rapid inspection of mechanical seals and bearings. However, maintaining strict suction piping geometry is critical, as air pockets in horizontal suction lines cause loss of prime.
Submersible Deep Well and Sump Units
Submerged units eliminate suction lift calculations and priming challenges by resting directly inside the water reservoir or borehole. A submersible clean water pump operates with low acoustic emissions and requires zero surface floor space. Ensuring continuous motor cooling through water flow jackets and monitoring dynamic water drawdown protects submerged motors against thermal damage.
Multi-Stage High-Pressure Booster Assemblies
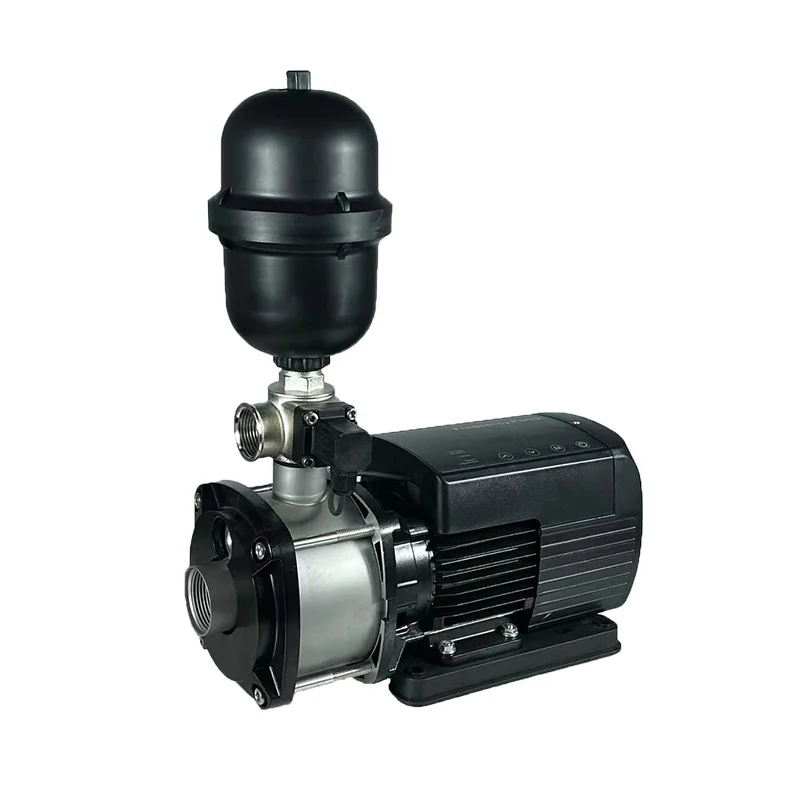
When agricultural drip lines or high-rise water systems demand elevated pressure without excessive volumetric flow, multi-stage units link multiple impellers in series within a single casing. This arrangement builds pressure incrementally, delivering high discharge head while maintaining balanced electrical consumption.
⚠️ Mitigating Inlet Friction and Cavitation Destruction
Cavitation represents the most destructive phenomenon in fluid mechanics, occurring when static pressure at the pump eye falls below the vapor pressure of the liquid. Vapor bubbles form instantly and collapse violently against metal surfaces, eroding impeller blades and shattering mechanical seals.
To protect an active clear water pump, system designers must verify that Net Positive Suction Head Available (NPSHa) exceeds Net Positive Suction Head Required (NPSHr) by a safety margin of at least 0.5 to 1.0 meter.
Suction Design Parameter
Common Field Defect
Recommended Piping Practice
Suction Pipe Sizing
Matching suction pipe to the pump intake diameter
Sizing intake line one nominal diameter larger to reduce intake velocity
Incline Toward Intake Port
Creating high spots that trap migrating air pockets
Maintaining an unbroken upward slope toward the clean water pump inlet
Inlet Pipe Straight Run
Installing sharp elbows directly against the pump suction flange
Providing straight pipe run equal to five to ten times pipe diameter
Foot Valve & Strainer Setup
Restrictive or silt-choked intake strainers
Selecting low-resistance foot valves with generous open mesh area
| Suction Design Parameter | Common Field Defect | Recommended Piping Practice |
|---|---|---|
| Suction Pipe Sizing | Matching suction pipe to the pump intake diameter | Sizing intake line one nominal diameter larger to reduce intake velocity |
| Incline Toward Intake Port | Creating high spots that trap migrating air pockets | Maintaining an unbroken upward slope toward the clean water pump inlet |
| Inlet Pipe Straight Run | Installing sharp elbows directly against the pump suction flange | Providing straight pipe run equal to five to ten times pipe diameter |
| Foot Valve & Strainer Setup | Restrictive or silt-choked intake strainers | Selecting low-resistance foot valves with generous open mesh area |
Correcting intake design prior to installation protects the clean water pump from continuous vibration, bearing destruction, and premature hydraulic failure.
🛡️ Mechanical Construction and Electrical Motor Defense
Continuous operating dependability depends heavily on internal metallurgy, dynamic balance, and electrical monitoring hardware. Sourcing units with heavy-duty construction prevents nuisance field shutdowns during seasonal peak demands.
Industrial environments demand motors rated for continuous duty with IP55 or IP68 environmental protection and Class F thermal insulation. Integrating automated dry-run protection via float sensors or digital current monitors ensures the clean water pump immediately shuts down if supply tanks empty, preventing mechanical seal face melting.
🏭 Manufacturing Precision and Global Supply Chain Excellence
Executing successful agricultural, industrial, and municipal water projects requires working with a verified production partner capable of delivering consistent hydraulic quality. For international distributors, civil contractors, and OEM brands, sourcing from a vertically integrated clean water pump manufacturer guarantees structural reliability and competitive wholesale advantages.
This is where Flyaway serves as an indispensable manufacturing leader across global fluid handling sectors. Operating state-of-the-art automated casting lines, computerized CNC precision machining centers, and automated digital testing bays, Flyaway engineers and manufactures a comprehensive portfolio of pumping machinery.
From single-stage end-suction units to multi-stage high-pressure solutions, Flyaway provides robust OEM and ODM manufacturing capabilities. Every clean water pump undergoes computerized hydraulic performance tests, dynamic impeller balancing, and strict hydrostatic pressure containment checks before export delivery. By pairing stringent quality control with seasoned export documentation and supply chain stability, Flyaway empowers global distributors to serve regional markets with dependable pumping assets engineered for long service lifecycles.
📋 Comprehensive Clear Water Procurement Matrix
Before signing commercial contracts or confirming engineering specifications, review this comprehensive selection verification matrix:
Procurement Stage
Technical Verification Focus
Ideal Engineering Outcome
Liquid Purity Verification
Sediment concentration, operating temperature, fluid pH
Proper wetted metallurgy and seal elastomer selection
Hydraulic Point Matching
System flow and Total Dynamic Head alignment with BEP
Maximized operational efficiency and minimized electrical draw
Intake Engineering
NPSHa calculation versus pump manufacturer NPSHr
Complete elimination of destructive hydraulic cavitation
Operational Protections
Overload relays, dry-run sensors, phase failure protection
Long-term motor winding and mechanical seal defense
Manufacturing Validation
Certified factory pump test curves and warranty records
Sourcing directly from Flyaway for validated quality
| Procurement Stage | Technical Verification Focus | Ideal Engineering Outcome |
|---|---|---|
| Liquid Purity Verification | Sediment concentration, operating temperature, fluid pH | Proper wetted metallurgy and seal elastomer selection |
| Hydraulic Point Matching | System flow and Total Dynamic Head alignment with BEP | Maximized operational efficiency and minimized electrical draw |
| Intake Engineering | NPSHa calculation versus pump manufacturer NPSHr | Complete elimination of destructive hydraulic cavitation |
| Operational Protections | Overload relays, dry-run sensors, phase failure protection | Long-term motor winding and mechanical seal defense |
| Manufacturing Validation | Certified factory pump test curves and warranty records | Sourcing directly from Flyaway for validated quality |
Following this systematic engineering framework ensures that every deployed centrifugal water pump delivers optimized efficiency, hydraulic stability, and predictable lifecycle valu